

Stronger fly ash blocks cannot be guaranteed with the raising of hydraulic pressure alone. A factory can raise forming pressure to produce smoother surfaces while still holding inner voids, chipping edges, inconsistent compressive strength, and layer separation.
Varied moisture content, poor particle grading, uneven filling of the mold, improper vibration settings, and inadequate curing lead to many quality issues. The evaluation of a Fly Ash Block Production Machine must be done in conjunction with the complete preparation, forming, handling, and curing of the material.
What Affects the Density and Strength of a Block?
The degree of packing of solid particles in a given volume defines Density, and is expressed as:
Dry density = Oven-dry mass ÷ Block volume
The general rule is that minimum density corresponds to maximum porosity, although it must be recognized that density is not the sole determinant of strength. Other factors include:
• Fineness and chemical activity of fly ash
• Content of cement, lime, gypsum and other binders
• Grading of aggregates
• Water/binder ratio
• Forming and demolding stability
• Curing conditions (temperature, humidity, time)
Excessive compaction can lead to layering and poor demolding. Buyers should assess both density and strength distribution rather than pursuing the highest possible pressure.
Evaluate Strength Consistency
Average compressive strength can hide unstable production. Quality evaluation should include:
• Minimum individual strength
• Standard deviation
• Coefficient of variation
• Seven-day and 28-day strength
• Batch-to-batch deviation
• Edge and corner integrity
The coefficient of variation is calculated as:
Coefficient of variation = Standard deviation ÷ Average strength × 100%
A lower value normally indicates more consistent batching, forming, and curing.
Raw Materials Must Be Evaluated First
A Fly Ash Block Production Machine cannot compensate for unsuitable or highly unstable materials.
Fly Ash Characteristics
Important variables include:
• Particle-size distribution
• Fineness
• Moisture content
• Loss on ignition
• Unburned carbon
• Reactive glass phase
• Chemical composition
• Variation between deliveries
High unburned-carbon content may affect water demand and binder interaction. Excessive fine material can improve void filling but also increase moisture demand and reduce feeding flow.
Particle Packing and Moisture
A well-graded mixture uses fine particles to fill spaces between larger particles. Poor grading can produce either excessive voids or a sticky mixture that is difficult to distribute.
For semi-dry forming, the optimum moisture level should be established through production trials. Operators should check whether the mixture:
• Forms a stable lump when compressed
• Breaks apart without smearing
• Fills corners and narrow mold sections
• Releases without sticking
• Maintains shape after demolding
Even a small moisture shift can change feeding behavior and green-block strength.
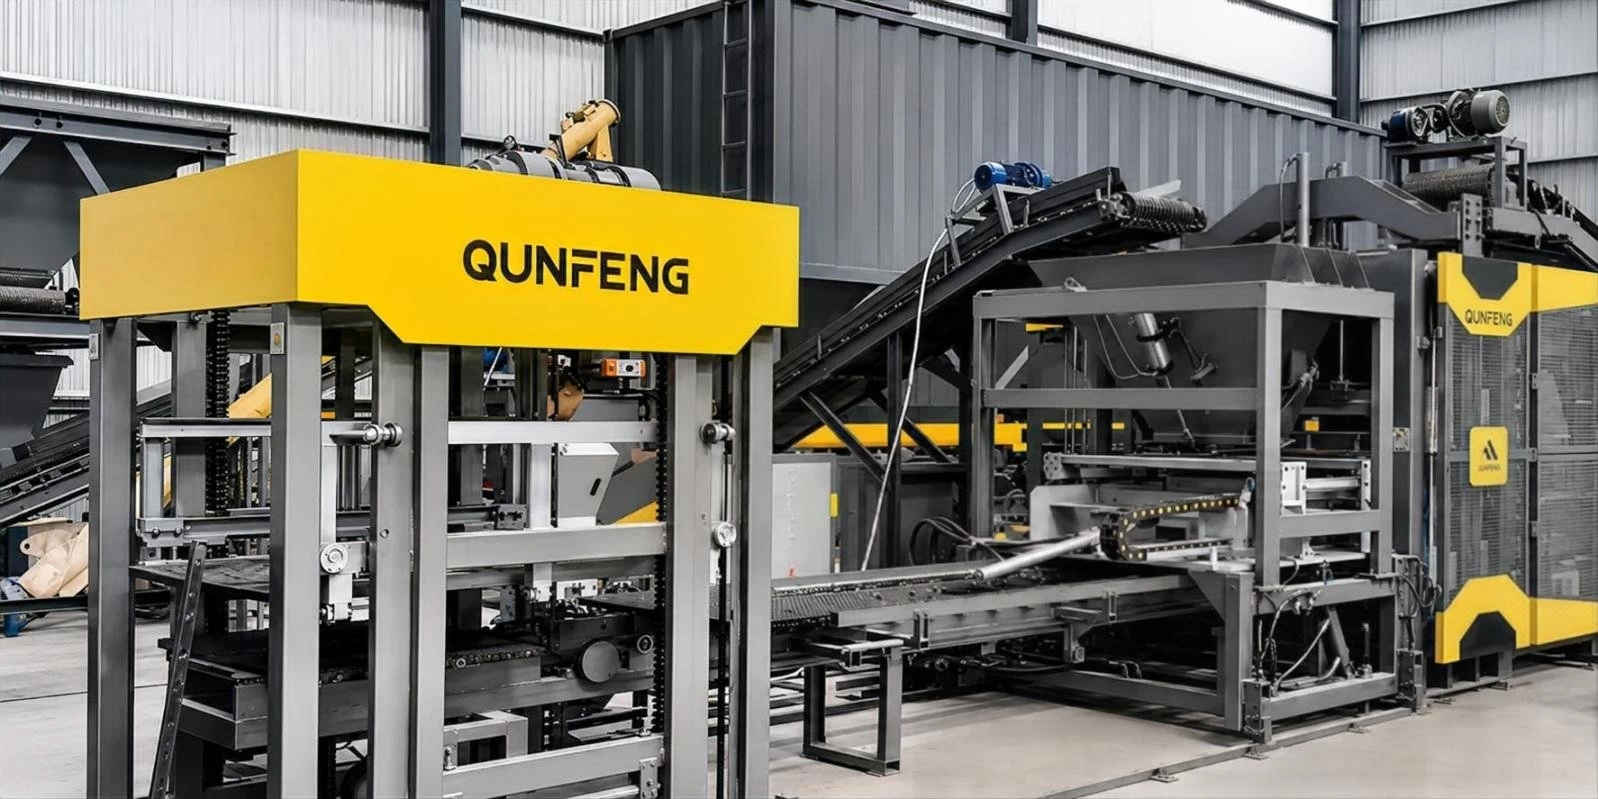
Comparison of Forming Technologies
Forming Technology | Operating Principle | Main Advantage | Limitation |
Mechanical vibration | Mechanical excitation with mold compression | Relatively simple structure | Limited parameter flexibility |
Vibration-hydraulic | Vibration rearranges particles before hydraulic consolidation | Suitable for blocks, blocks, and pavers | Requires coordinated pressure and vibration |
Servo vibration-hydraulic | Servo-controlled frequency, response, and forming stages | High parameter repeatability | Higher control and maintenance requirements |
Static high-pressure pressing | High static pressure without intensive vibration | Suitable for certain solid products | Less flexible for complex or hollow products |
No single technology is suitable for every plant. Selection should depend on product geometry, raw-material grading, target density, production volume, mold-change frequency, power availability, and local maintenance capability.
How Vibration and Pressure Work Together
Effect of Vibration on Particle Arrangement
In the process of forming, vibration is an important element as it decreases the internal friction of particles, allowing them to:
• Move and fill the mold cavity
• Minimize localized voids
• Release trapped air
• Spread and fill the mold cavity
• Create a uniform layer prior to pressing
In Fly Ash Block Production Machines, some fixed frequency vibrations can work for individual products, but it is better to use a wider adjustable range for some flexibility to deal with various materials and dimensions of blocks.
Hydraulic Pressure Completes Consolidation
Hydraulic pressure limits product height, increases green strength, and improves edge definition. However, rated system pressure is not the same as the pressure acting on the block surface.
Actual forming force is influenced by:
• Cylinder effective area
• Press-head area
• Number of mold cavities
• Hydraulic losses
• Pressing stroke
• Material resistance
• Pressure-holding time
A controlled forming sequence normally includes feeding, pre-vibration, press-head descent, main vibration, hydraulic compression, short holding, and synchronized demolding.
Comparison of Machine Capabilities
Two vibration-hydraulic machines may have similar rated capacities but very different control depths.
Control Area | Basic Machine | Advanced Machine | Production Effect |
Vibration | Fixed setting | Adjustable frequency and stages | Better density consistency |
Hydraulic control | Basic pressure limit | Pressure and sequence monitoring | Lower height variation |
Feeding | Simple reciprocating feeder | Rotary rake or multi-stage feeding | More uniform mold filling |
Press head | Basic guidance | Multi-cylinder synchronized guidance | More even compression |
Mold system | Standard machining | Heat-treated plates and hardened guides | Longer dimensional stability |
Data management | Output counter | Pressure, downtime, and alarm records | Improved traceability |
Key Parameters Buyers Should Compare
Parameter | Technical Reference | Procurement Importance |
Vibration frequency | Adjustable range under load | Affects particle movement |
Rated pressure | System pressure and force transmission | Affects forming repeatability |
Cycle time | Must match the actual product | Determines realistic capacity |
Product height range | Minimum and maximum forming height | Indicates product flexibility |
Pallet size | Effective molding area | Determines pieces per cycle |
Feeding method | Feeder path and distribution structure | Affects block-weight variation |
Mold-change time | Measured production stoppage | Important for multi-product plants |
Installed power | Main machine and complete line separately | Supports energy-cost calculation |
Calculate Qualified Output
Rated capacity should be converted into qualified production:
Qualified output = Pieces per pallet × Actual cycles per hour × Utilization × Pass rate
For example, a Fly Ash Block Production Machine producing 70 blocks per pallet at a 15-second cycle has a theoretical output of:
• 3,600 ÷ 15 = 240 cycles per hour
• 240 × 70 = 16,800 blocks per hour
• At 85% utilization and a 97% pass rate:
• 16,800 × 0.85 × 0.97 ≈ 13,852 qualified blocks per hour
High-strength products may require longer feeding, vibration, or holding time. The shortest cycle is therefore not always the most economical setting.
Qunfeng Technical Reference
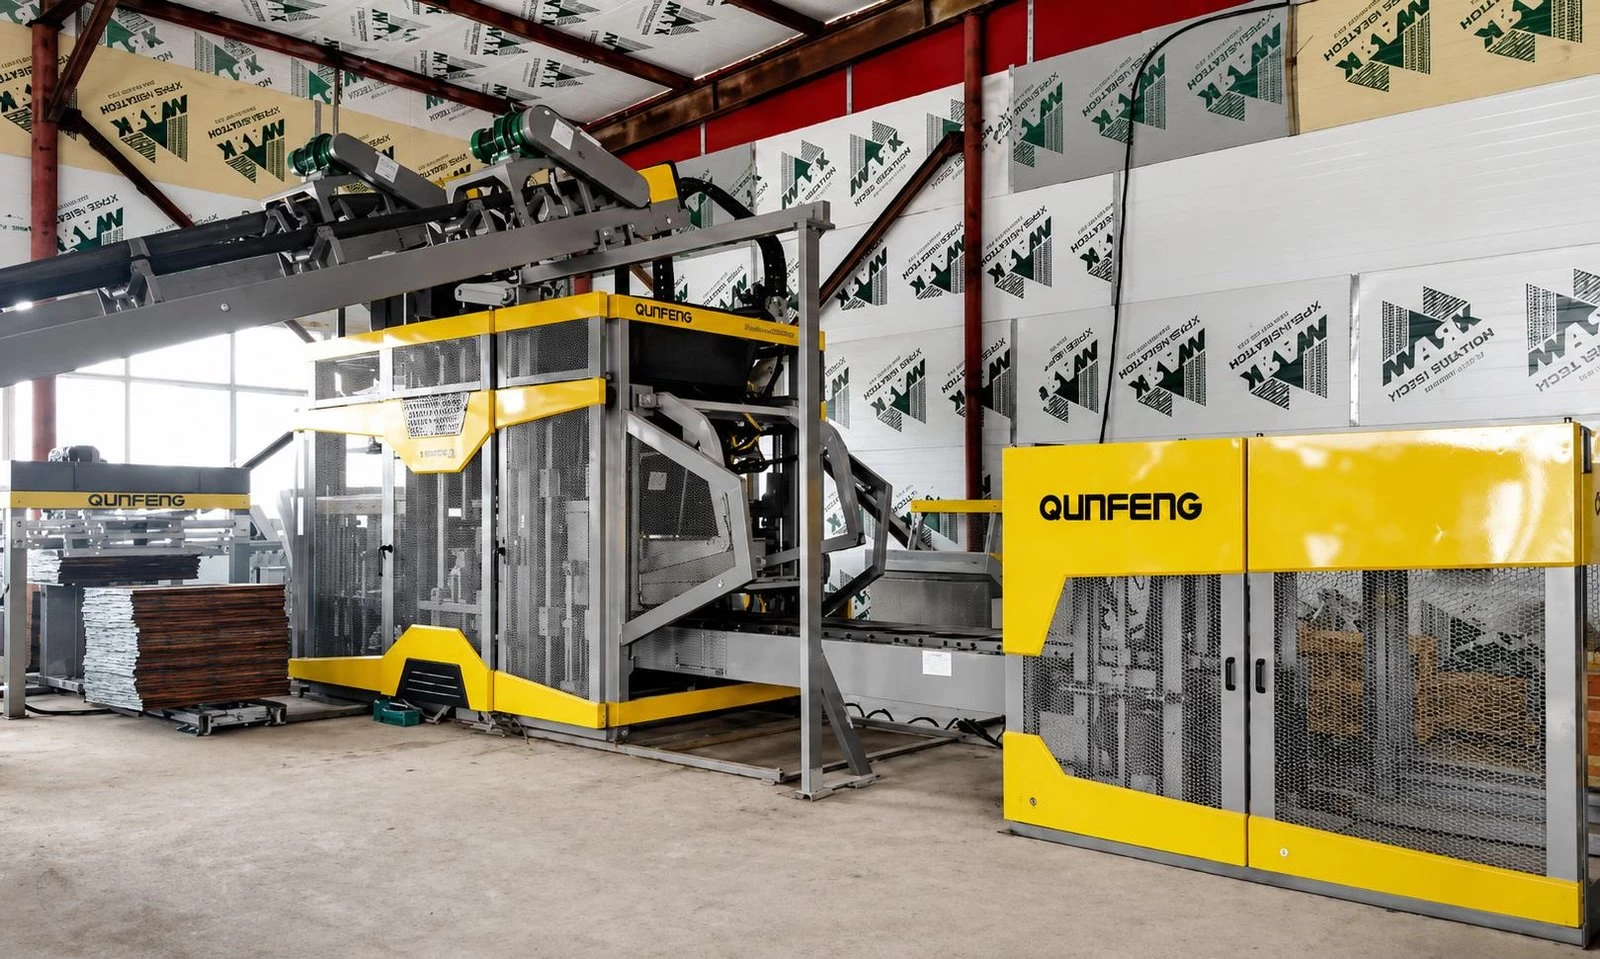
Qunfeng's QS1500 can be used as a technical reference for comparing servo-based forming systems. Manufacturer-provided specifications include:
• Four-axis servo vibration
• Frequency range of 0–75 Hz
• Rated hydraulic pressure of 21 MPa
• Forming a cycle of 11–19 seconds
• Product height range of 35–300 mm
• Pallet size of 1,400 × 1,000 mm
• Main-machine installed power of 87.1 kW
The adjustable vibration range supports parameter matching for different materials and product heights. Its 360-degree rotary rake feeder is intended to improve multi-cavity filling, while the dual-cylinder press-head structure supports synchronized compression. Heat-treated mold plates, strong guide pillars, airbag clamping, and vibration isolation help keep the dimensions stable and make it easier to change molds.
Closing Words
High-density and high-strength blocks result from coordinated raw-material preparation, moisture control, feeding, vibration, pressure, demolding, and curing. Buyers should compare different options side by side to choose a forming method and look at how well each option controls depth, mold accuracy, feeding consistency, and traceability.
Are you considering the establishment of a Fly Ash Block Production Machine project? Send Qunfeng your fly ash data, binder system, product dimensions, desired compressive strength, curing method, and expected output. Following this, the trials for production, along with the variations in parameters, will allow the proposal of technically matched equipment.
FAQs
Q1. What materials can be processed using a Qunfeng Fly Ash Block Production Machine?
A Qunfeng Fly Ash Block Production Machine may be configured for a variety of combinations including fly ash, cement, sand, stone powder, slag, tailings, and some recycled aggregates. The mixtures should be determined by testing the materials locally.
Q2. How does Qunfeng enhance the density of fly ash blocks?
Qunfeng employs controlled material feeding, servo vibration, and hydraulic compression with a system for synchronized demolding. This technology helps to evenly distribute the material and eliminate internal voids to enhance density.
Q3. Do stronger blocks require higher hydraulic pressure?
Not necessarily. Hydraulic pressure is one of many variables that affect block strength. Other variables include the moisture content, particle grading, binder activity, vibration, uniformity of the feeding, precision of the mold, and the conditions of curing.
Q4. What is the vibration frequency range of the Qunfeng QS1500?
The Qunfeng QS1500 is equipped with a four-axis servo vibration system. The specified frequency range is 0–75 Hz. Actual settings should be determined based on the material, the height of the block, the structure of the mold, and the density of the block.
Q5. What is the maximum height of products that can be formed using the Qunfeng QS1500?
The maximum height that can be formed using the Qunfeng QS1500 is in the range of 35–300 mm. Thus, thin paving units, standard blocks, concrete blocks, and curbstones can be formed, along with other concrete products using appropriate molds.